
China Top 10 Laser Quenching Machine Manufacturers
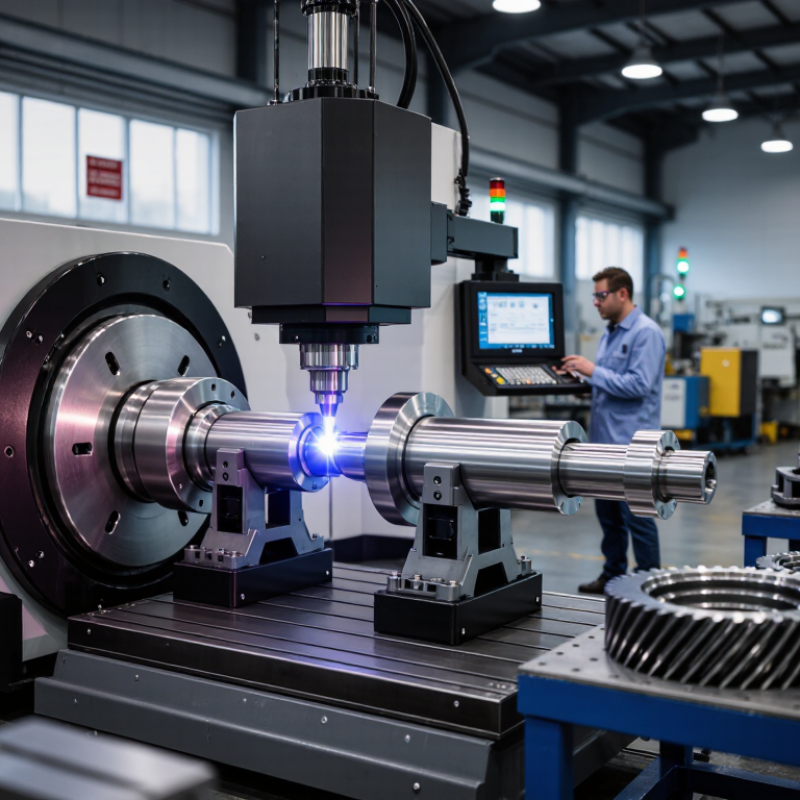
Choosing a Laser Quenching Machine is not just a matter of comparing power ratings. The right system must deliver repeatable surface hardening, fit the component geometry, and integrate with the factory’s production line. A shaft rotating beneath a focused beam presents different demands from a broad gear tooth or a complex automotive part. Small differences in beam control, scanning speed, and cooling can affect hardness and distortion. Details matter.
Laser-processing expert William M. Steen’s published work provides a useful foundation, but I cannot verify a verbatim quotation from him for this article. A practical paraphrase of the engineering principle is: “Match the laser process to the material, geometry, and required surface properties.” Treat that as a paraphrase, not a direct quote. It is a reminder to ask manufacturers for process data, sample trials, and clear specifications—not simply a catalogue promise.
This guide reviews China’s top 10 laser quenching machine manufacturers through practical buying criteria, including equipment capability, customization, quality controls, technical support, and export experience. Look for evidence: a test report, a documented hardness profile, and a realistic service plan. A polished brochure helps, but it cannot replace a production trial. Some comparisons may remain imperfect because suppliers publish different levels of technical detail. Readers should verify claims directly and assess each machine against their own parts, materials, and production targets.
Laser Quenching Basics: 10³–10⁵ W/cm² Power Density and Self-Quenching
Laser quenching concentrates energy into a narrow surface zone, often at power densities around 10³–10⁵ W/cm². The exact setting depends on the alloy, beam size, surface condition, and travel speed. The range is broad. A small change in focus can shift the heated track from shallow to uneven.
As the beam moves, the surface heats rapidly, while the cooler material beneath it acts as a heat sink. Once the laser passes, heat flows inward and cools the surface without a separate quenching bath. This is self-quenching. If the steel’s composition and thermal cycle are suitable, the transformed surface can develop a hard martensitic layer, while the core remains tougher. Timing matters. Too little energy may leave soft patches; too much can cause melting, roughness, or excessive distortion. In practice, operators check power, spot size, and scan speed together, then inspect hardness and case depth on test pieces. A power-density figure alone cannot predict the result. I would treat it as a starting point, not a recipe; that distinction is easy to overlook.
