Why Choose Taped Litz Wire for High Frequency Applications?
At high frequency, a coil can lose useful energy as current crowds toward the conductor’s surface. taped litz wire addresses this challenge with many fine, insulated strands bundled together and wrapped with tape. Picture a compact transformer winding: dozens of slender copper paths, held in place by a smooth outer layer. The design can reduce AC resistance and help manage winding losses. It is not a universal fix.
Charles R. Sullivan, a researcher known for work on magnetics and litz-wire design, has studied how strand dimensions affect winding losses. A practical paraphrase of his research is: “Match strand size and winding design to the operating frequency.” This is a summary, not a verbatim quotation. That distinction matters when engineering decisions depend on evidence.
Why choose taped litz wire for high frequency applications? This introduction explores the balance between electrical performance, insulation, and manufacturability. Tape can provide a consistent barrier and help a winding retain its shape. Yet it also adds thickness, and poor strand selection can undermine the expected benefit. Small details matter. Frequency, conductor size, winding geometry, and thermal conditions all shape the result. Sometimes a simpler conductor is the better choice. That deserves a closer look.
The sections ahead explain where taped litz wire can help, what to check when specifying it, and which trade-offs deserve attention. Engineers should verify performance in the intended assembly, not rely on a material label alone. Real windings can behave differently than neat calculations predict.
What Taped Litz Wire Is and How It Is Constructed
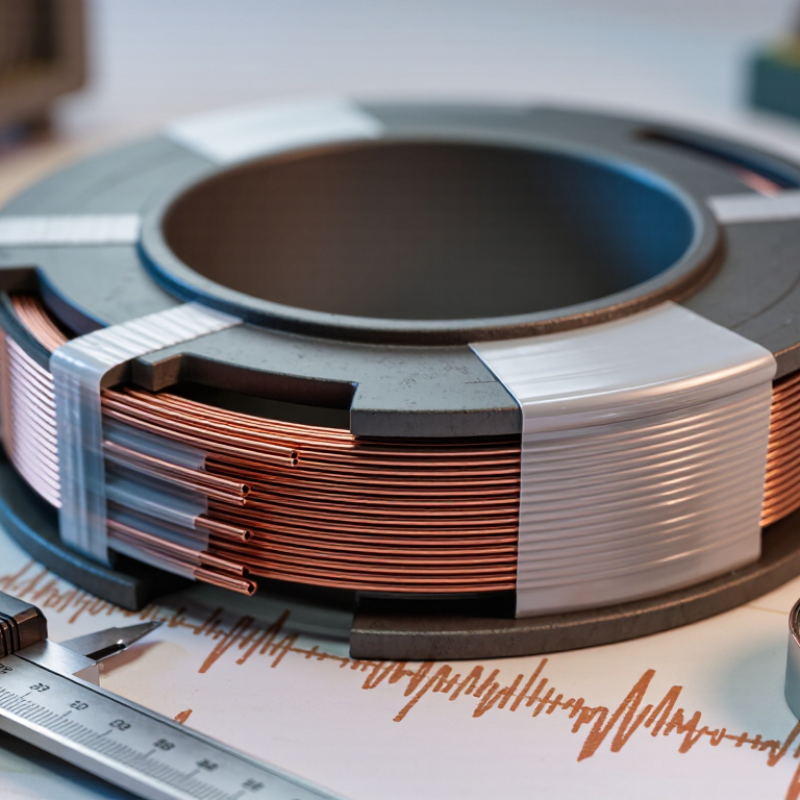
Taped litz wire combines many fine, individually insulated copper strands with a protective outer wrap. The strands are bundled or braided so their positions change along the cable. This transposition helps each strand experience a more even share of the magnetic field. At higher frequencies, that can reduce skin-effect and proximity-effect losses compared with a solid conductor of similar copper area.
The tape is applied around the completed strand bundle. Depending on the design, it may be polyester, polyimide, or another specified insulating material. It helps hold the bundle together and adds a layer of electrical and mechanical protection. It does not replace strand insulation, and it does not automatically reduce electrical losses. Small details matter. Tape overlap, strand diameter, and winding space can affect how the wire performs in a real coil. Selection should match the operating frequency, temperature, voltage, and available space.
Tips: Check the wire’s construction and insulation ratings against the coil design. A thicker wrap may improve handling, but it can also make winding less convenient. It is not a magic fix; prototype testing can reveal issues calculations miss.
