How to Choose the Right Injection Molding Die in 2026?
Choosing the right Injection Molding Die in 2026 requires more than comparing supplier prices. It demands a careful reading of material behavior, part geometry, production volume, and expected service life. Grand View Research valued the global injection molding machine market at approximately USD 20.6 billion in 2023. It also projects continued growth through 2030. That expansion increases pressure on manufacturers to reduce waste, downtime, and tooling mistakes.
The numbers are significant. PlasticsEurope reported global plastics production of about 413.8 million tonnes in 2023. Every molded component carries practical consequences. A thin automotive panel may need balanced cooling and controlled warpage. A medical housing may require polished cavities, strict traceability, and repeatable dimensions. An Injection Molding Die that performs well for polypropylene may fail with glass-filled nylon. Material selection changes everything.
John Bozzelli, founder of Scientific Molding, often emphasizes, “The mold is the heart of the injection molding process.” His point remains highly relevant. The die controls filling, cooling, ejection, and much of the final part quality. Yet no selection formula is perfect. A low-cost die can become expensive after repeated repairs. A sophisticated die can also be excessive for a short production run. I would challenge the common assumption that the cheapest quotation is the safest choice. The better decision compares total ownership cost, maintenance access, cooling efficiency, steel grade, and supplier experience. This guide examines those factors for 2026, while recognizing that real production data should always challenge initial assumptions.
What Is an Injection Molding Die and How Does It Work?
How to Choose the Right Injection Molding Die in 2026?
What Is an Injection Molding Die and How Does It Work?
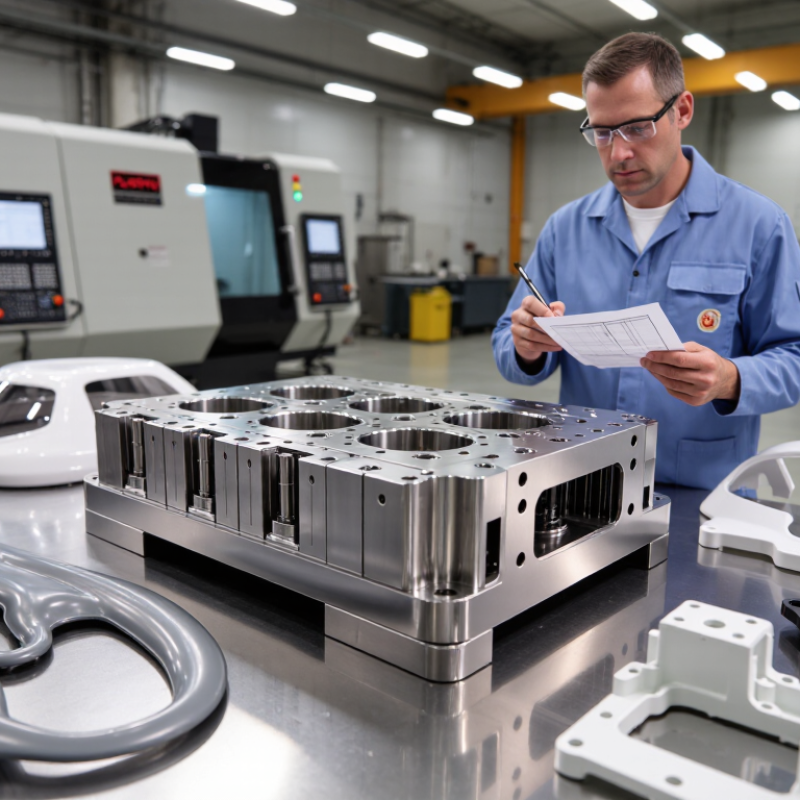
In injection molding, a die is the engineered tool that shapes molten plastic into a finished part. Many engineers call it a mold. Both terms describe a similar production tool. The die contains a cavity and a core, which create the part’s external and internal surfaces. Heated plastic enters through the sprue, runner, and gate. Cooling channels then remove heat from the steel or aluminum tool. After solidification, ejector pins release the molded component.
A suitable die must match the resin, part geometry, production volume, and machine capacity. For example, glass-filled material can accelerate wear around gates and corners. Deep ribs may require carefully positioned slides or lifters. Thin walls need balanced filling and controlled cooling. Otherwise, warping, sink marks, or short shots may appear. Small details matter.
Practical tooling reviews often begin with flow analysis, steel selection, and maintenance access. A hardened tool may cost more initially, but it can withstand repeated cycles better. Aluminum tools can support faster prototype work, although their service life may be shorter. I have seen attractive designs fail because technicians could not clean narrow cooling passages easily. That mistake is easy to overlook. In 2026, sensors can monitor pressure, temperature, and cycle variation, but data cannot fix poor gate placement. Engineers should test the first articles, inspect dimensions, and question assumptions before approving full production.
