How to Choose the Best CNC Cutting Tools?
Choosing the right Cnc Cutting Tools is not a catalog exercise. It is a production decision that affects cycle time, surface finish, tool life, and scrap risk. The Grand View Research report on the global CNC machine market estimated its value at $101.22 billion in 2023 and projected a 9.8% compound annual growth rate from 2024 to 2030. That figure describes CNC machines, not cutting tools, but it signals a growing machining environment where tool selection matters. A busy shop floor makes the consequences visible: chipped edges, heat-darkened chips, and a spindle waiting while an operator changes a tool.
Start with the material, operation, machine, and production goal. A carbide end mill suited to aluminum may not perform well in stainless steel. Coating, geometry, flute count, and tool-holder rigidity all influence results. So does coolant delivery. Professor Tony Schmitz, a machining researcher at the University of Tennessee, studies the dynamics behind cutting processes. His work supports a useful selection principle: evaluate the tool as part of the complete machining system, rather than in isolation. Check the machine’s power and speed limits, then compare supplier data with a controlled shop test.
Small details matter. A few microns of runout can shorten tool life. Measure the first part. Inspect the chips. Record wear and cycle time. Then adjust.
This guide explains how to compare tool materials, coatings, geometries, and costs. It also highlights common selection mistakes, so buyers can make decisions based on verified performance—not a promising label alone.
Define the CNC Cutting Task and Its Requirements
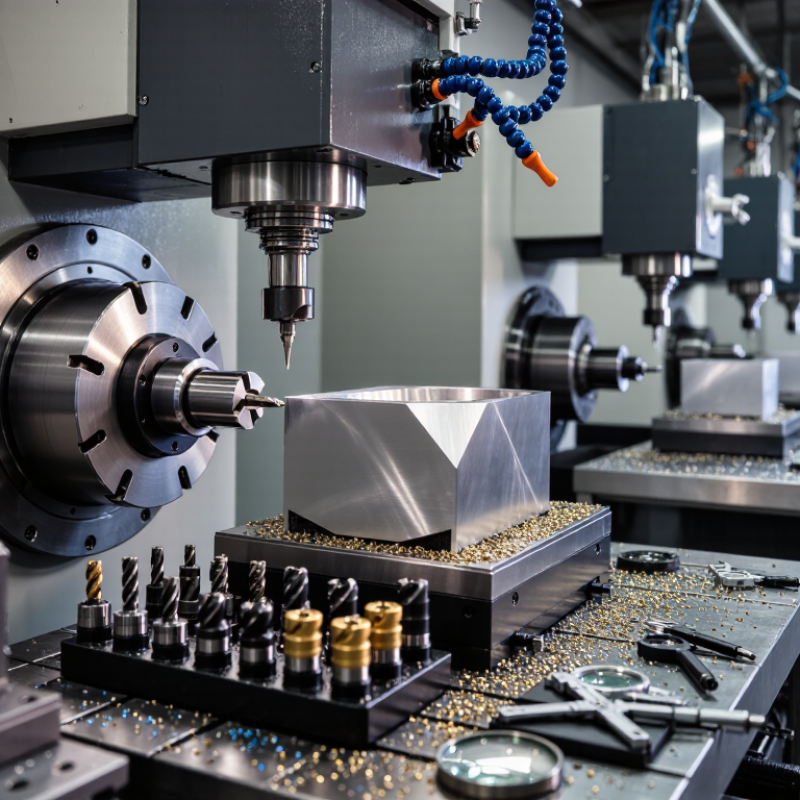
Before choosing a CNC cutting tool, define the job in measurable terms. Name the exact material and hardness, then record the operation: roughing, slotting, drilling, or finishing. A vague label like “stainless steel” is not enough; grade and work-hardening behavior can change the choice. Note the stock shape, allowance, target tolerance, surface finish, and production quantity. A 0.02 mm tolerance on a thin wall demands different planning from roughing a solid block.
Check the machine as carefully as the part. Record spindle speed and torque limits, tool reach, holder clearance, setup rigidity, coolant delivery, and how chips will leave the cut. A long tool may reach the pocket, but vibration can spoil the finish. I would verify the setup with a trial cut; the first estimate can be wrong. Small details matter.
Include operator exposure and fluid management in the requirements. NIOSH’s Criteria for a Recommended Standard: Occupational Exposure to Metalworking Fluids (1998) gives recommended exposure limits of 0.4 mg/m³ for thoracic particulate and 0.5 mg/m³ for total particulate, as time-weighted averages. These are U.S. recommendations, not universal legal limits or tool-selection thresholds. Still, they make coolant choice, mist control, and enclosure performance relevant to the process plan. Define these constraints before comparing tool geometry or coating.
