
How to Choose POY Spinning and Winding Machines?
Polyester dominates modern filament production, making POY line choices a practical investment decision. Textile Exchange’s Materials Market Report 2024 estimates that global fiber production reached 124 million tonnes in 2023, with polyester representing about 57%. This scale creates pressure for consistent output, reliable quality, and efficient production. But market size alone cannot tell a mill which machine to buy.
POY Spinning And Winding equipment must match the intended yarn specifications and factory conditions. Start with polymer throughput, filament count, denier range, and required winding speed. Then examine extruder stability, quenching uniformity, godet control, and package formation. These details show up on the shop floor: uneven cooling can affect yarn consistency, while unstable winding can produce packages that unwind poorly downstream. Small details matter.
Compare suppliers using documented performance data, not headline speed alone. Request trial results for your target polymer and yarn, including breakage rates, package weight consistency, energy use, and changeover time. Check spare-part availability, operator training, control-system access, and service response times. A faster line may not improve output if maintenance interruptions or downstream rejects increase. That is easy to overlook. Textile Exchange reports fiber-market scale, not machine-level performance; buyers should treat its figures as context, not proof of equipment capability. Some specifications still need verification on the buyer’s own material. A careful trial, with clear acceptance criteria, can reveal what a brochure cannot.
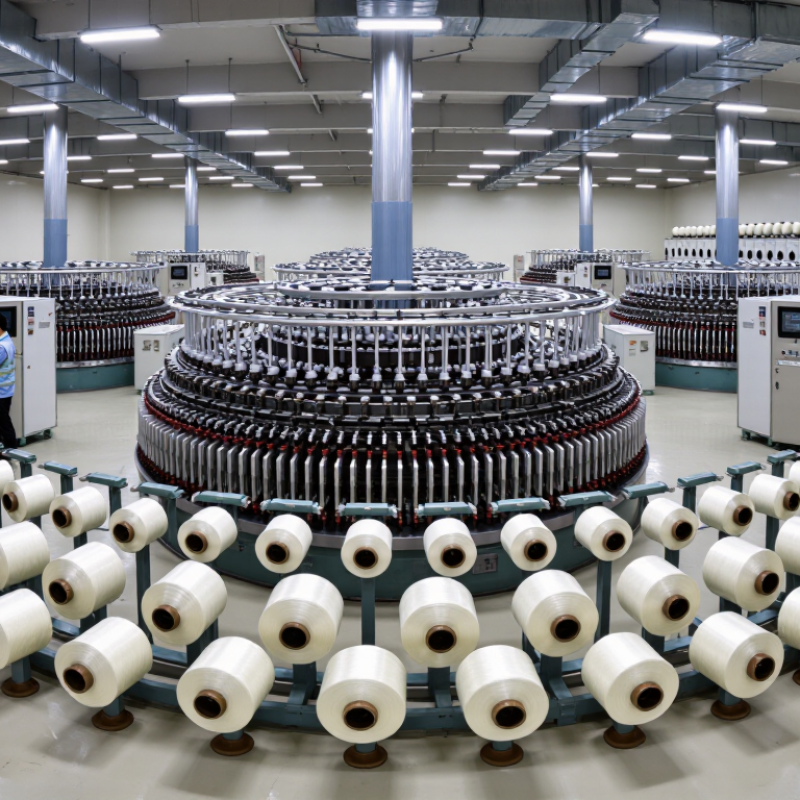
Understanding POY Production Requirements and Machine Functions
POY line selection starts with the yarn you need to deliver, not the machine’s headline speed. Define polymer type, target denier, filament count, number of ends, and package size. These determine the metering-pump output, spinneret layout, quench capacity, and winding positions. Textile Exchange’s Materials Market Report 2024 estimates global fiber production at 124 million tonnes in 2023, with polyester representing about 57%. That scale makes polyester context relevant, but it does not prescribe a POY line’s settings.
Watch the yarn’s path. Melt flow must remain steady through the spinneret; controlled cooling helps form consistent filaments. Finish application and godet speed influence handling and orientation, while the winder must manage tension and traverse to build packages that unwind reliably during draw texturing. Ask suppliers for trial data using your polymer and target yarn, including breaks, package density, and doff time. Small differences matter. A tidy package can still hide uneven tension. Match throughput to downstream demand, too; an oversized line may look efficient on paper but create inventory and quality headaches. Machine brochures rarely show the whole operating picture, and that deserves a second look.
| Selection Dimension | Production Requirement | Relevant Machine or Function | What to Check When Choosing |
|---|---|---|---|
| Polymer and feed preparation | Consistent, clean polymer melt is essential for stable filament formation. PET production also requires moisture control because excessive moisture can degrade the polymer during melt processing. | Dryer and conveying system, extruder, melt filtration, and melt delivery components. | Confirm compatibility with the intended polymer, drying and conveying requirements, filtration arrangement, melt-temperature control, and the supplier’s recommended operating limits. |
| Yarn product specification | Define the target yarn type, total denier or dtex, filament count, number of ends, and intended downstream use before selecting a machine configuration. | Metering pumps, spinnerets, spinning positions, and winding positions determine how the yarn is formed and collected. | Ask for a configuration matched to the required products. Denier, filament count, polymer properties, and process settings affect achievable output and package quality. |
| Spinning capacity | Required output depends on the number of spinning positions, yarn specification, polymer throughput, and operating conditions. | Extruder capacity, melt distribution, metering pumps, and position layout. | Compare rated capacity with the intended product mix, and request capacity figures for the specific yarn specifications rather than relying on a single headline output value. |
| Spinneret and filament formation | Spinneret design and condition influence filament count, filament uniformity, and the stability of the emerging filaments. | Spin pack, filter media, spinneret, and associated heating and sealing components. | Check spinneret options, changeover and cleaning procedures, spare-part availability, and the filtration arrangement recommended for the polymer and product. |
| Quenching and cooling | Filaments need controlled cooling after extrusion to support consistent solidification and yarn properties. | Quench-air system, air distribution components, and environmental controls around the spinning cabinet. | Review air-flow uniformity, filtration, temperature and humidity management, and accessibility for inspection and maintenance. |
| Spin finish application | Finish helps control friction and static during yarn handling and subsequent processing. The required finish depends on the yarn and downstream process. | Finish applicator, metering arrangement, and finish supply system. | Check application consistency, adjustment range, cleaning access, and compatibility with the chosen finish and downstream process. |
| Take-up speed | POY is wound at a partially oriented state for further processing, such as drawing or texturing. Production speed must suit the yarn specification and process stability. | Take-up winder, drive system, yarn path, and any godets included in the line design. | Many POY systems operate in the approximate range of 2,500–3,500 m/min, but actual suitable speeds vary by product and machine design. Verify the guaranteed range for the required yarn specification. |
| Winding package quality | Packages should have consistent build and stable unwinding performance for downstream use. | Winder, traverse mechanism, tension control, and package-change system. | Evaluate package dimensions and weight, winding pattern, tension stability, doffing method, and the ability to maintain package quality across positions. |
| Position-to-position consistency | Consistent yarn properties across positions help reduce variation in downstream processing. | Central process controls, individual position controls, and monitoring or alarm systems. | Ask which process variables are monitored, how alarms are recorded, and how operators can identify and correct position-level deviations. |
| Automation and operation | Automation can reduce routine handling and support repeatable production, but the required level depends on staffing and factory workflow. | Automatic doffing, package handling, recipe management, and operator interface. | Match automation to the plant layout and labor plan. Confirm changeover steps, operator training needs, and access to production data. |
| Utilities and plant layout | Machine performance depends on suitable power, compressed air, cooling, ventilation, and a layout that allows safe access. | Machine electrical and utility systems, cabinet ventilation, and installation layout. | Request utility consumption and connection requirements, foundation and clearance drawings, environmental requirements, and installation conditions before finalizing the layout. |
| Maintenance and spare parts | Planned maintenance and timely replacement of wear components help limit unplanned production interruptions. | Accessible service points, replaceable components, diagnostic functions, and recommended spare-parts package. | Review maintenance intervals, required tools, service support, critical spares, and the availability of operating and maintenance documentation. |
| Acceptance and performance verification | Machine performance should be demonstrated using agreed product specifications and operating conditions. | Factory and site acceptance procedures, measurement equipment, and production records. | Agree in advance on test yarn specifications, operating speed, package criteria, measurement methods, and the conditions used to evaluate output and quality. |
