How to Choose a Belt Measuring Tool for Accurate Sizing
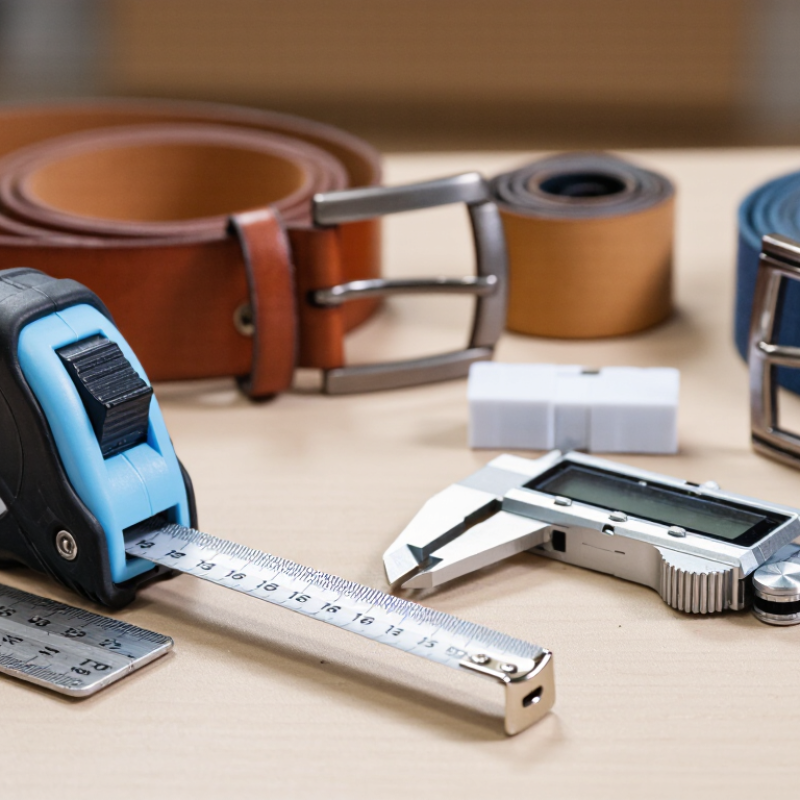
Choosing a Belt Measuring Tool starts with understanding what you need to measure: a loose belt, a belt fitted around a machine, or a replacement part. These situations call for different methods. A flexible tape can follow a curved path, while a rigid ruler may work better for a straight, accessible belt. The tool should also match the belt’s width and material. A narrow belt can twist under pressure, and a stiff belt may not sit flat. Small details matter.
Accuracy depends on more than the markings on the tool. Check whether its scale uses millimeters, inches, or both, and confirm that the zero point is easy to locate. For repeat measurements, use the same contact points and avoid stretching a flexible belt. If the tool has a calibration feature, follow the manufacturer’s instructions. Then compare a reading with a trusted ruler when practical. It is a simple check, but it can reveal a worn edge or confusing scale.
This guide explains how to compare common tool types, measure consistently, and choose a suitable option for your task. It also considers durability, readability, and ease of handling in real working conditions. A more expensive tool is not automatically better. Sometimes the simplest tool is enough. Still, I would not treat every measurement as exact; belt shape, tension, and user technique can affect the result. The aim is a reliable fit, not false precision.
Identify the Belt Type: ISO 4184 Covers V-Belt Length Designations
A belt’s printed number is meaningful only when its belt type and length system are known. ISO 4184 covers length designations and tolerances for classical and narrow V-belts. It uses datum length, marked Ld, as the reference. A tool reading the belt’s outside circumference may show a different value.
Look for the profile marking, such as A or SPA, before measuring. These profiles are not interchangeable, even when their widths seem close. Then check whether the tool measures datum length or another circumference. Read its instructions carefully. Small differences matter. A belt stretched around measuring pulleys can settle differently if it is twisted or not seated evenly.
Clean the belt and inspect its markings under good light. If they are worn, measure the cross-section at several points and compare it with the correct profile chart. Use a tool designed for V-belts, and keep the belt aligned without forcing it. Record the profile and the tool’s length reading together. One detail can be easy to miss: wear, heat, or a damaged edge may distort the measurement. When readings disagree, recheck the setup rather than choosing the closest number.
| Belt Profile | Nominal Top Width | Recommended Measuring Tool | What to Measure | Sizing Guidance |
|---|---|---|---|---|
| Classical Z | 10 mm | Profile gauge, followed by a calibrated belt length measuring machine | Confirm the cross-section, then measure the belt’s standardized datum length (Ld). | Use the Z profile designation when the belt’s section matches the classical Z profile. Do not identify length from the top width alone. |
| Classical A | 13 mm | Profile gauge and belt length measuring machine | Check the belt profile and record its datum length under the measuring machine’s specified conditions. | ISO 4184 length designations apply to classical and narrow V-belts; confirm the profile before comparing length markings. |
| Classical B | 17 mm | Profile gauge and belt length measuring machine | Measure the datum length rather than relying on a loose belt’s outside circumference. | Replace like-for-like by matching both the section and the applicable length designation. |
| Classical C | 22 mm | Profile gauge and calibrated belt length measuring machine | Verify the cross-section and measure the belt using the machine’s specified tension and procedure. | A belt that appears similar in width may have a different profile; check the sidewall and section dimensions. |
| Narrow SPZ | 9.7 mm | Profile gauge and belt length measuring machine suitable for narrow V-belts | Confirm the narrow profile and measure the designated datum length. | SPZ is a narrow V-belt section, not an alternative name for classical Z. Check the profile marking carefully. |
| Narrow SPA | 12.7 mm | Profile gauge and belt length measuring machine suitable for narrow V-belts | Record the profile and measured datum length; use the instrument’s prescribed setup. | Do not select a replacement using length alone if the existing belt’s section has not been identified. |
| Narrow SPB | 16.3 mm | Profile gauge and calibrated belt length measuring machine | Measure the standardized length and verify the belt’s cross-section independently. | Use an instrument and measuring procedure appropriate for the belt section; avoid comparing measurements taken under different conditions. |
| Narrow SPC | 22 mm | Profile gauge and calibrated belt length measuring machine | Confirm the SPC profile, then obtain the datum-length measurement with the specified machine setup. | Keep the section designation and length designation together when recording or ordering a belt. |
| Measurement note: A flexible tape can help with a preliminary check on a removed belt, but it may not reproduce a standardized datum-length measurement. Belt tension, wear, and measurement method can affect the result. For accurate identification, verify the profile and use the applicable ISO 4184 length designation and a suitable calibrated measuring method. | ||||
