China Best Glass Sorting Machine Manufacturer?
Choosing the best Glass Sorting Machine manufacturer in China is not as simple as comparing price lists. The right supplier should understand your feed material, target purity, required throughput, and plant conditions. A line handling clear container glass may need different settings from one sorting mixed-color cullet. Small details matter. Dust, uneven lighting, and fluctuating particle sizes can affect sorting performance.
A useful evaluation starts with evidence, not promises. Ask for a trial using representative glass samples, and review the results for color separation, contaminant removal, and usable output. Request clear specifications for capacity, air consumption, sensor configuration, and maintenance access. If possible, inspect a machine in operation and speak with existing customers processing similar material. Good technical support matters too; response times and spare-part availability can shape long-term operating costs. The numbers need context.
This guide examines how to compare Chinese manufacturers, what questions to ask, and which claims deserve closer checking. It also considers installation, operator training, warranty terms, and after-sales service. No single machine suits every recycling plant, and a polished brochure cannot replace a practical test. Some specifications may look impressive on paper. Verify them against your own material and production goals before making a decision.
Glass Sorting Machines: Purpose, Types, and Core Components
Glass sorting machines separate mixed cullet by color, size, shape, or material type. They help processors produce cleaner feedstock for remelting and reduce unwanted pieces in the output. Clean, consistent feed matters. Green, amber, and clear glass may need separate streams, while ceramics and heat-resistant fragments can be difficult to spot by eye.
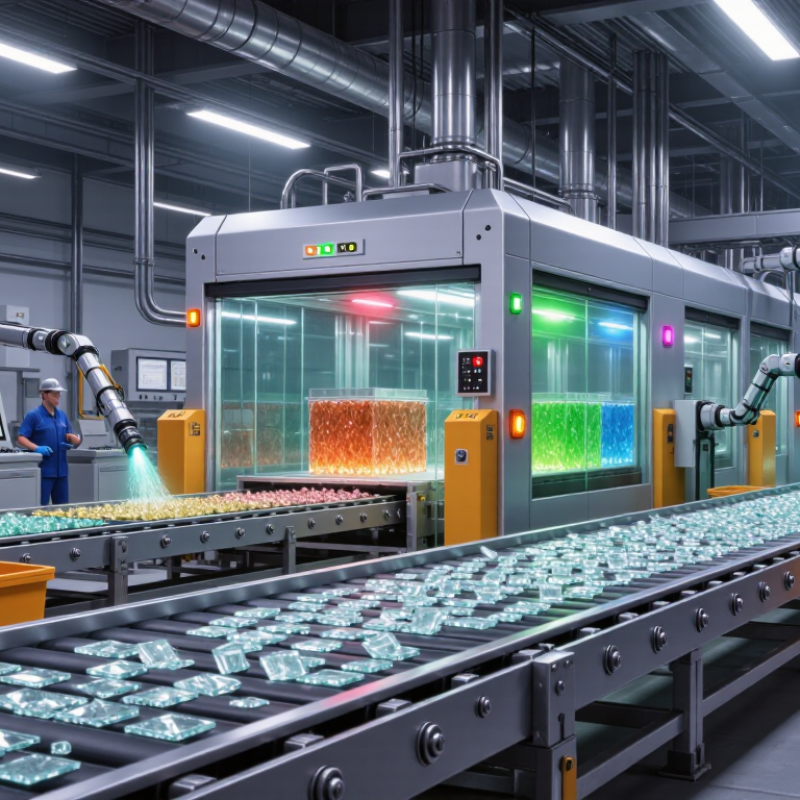
Optical color sorters use cameras or sensors to inspect glass as it travels along a belt or chute. Other systems detect contaminants through differences in material properties. A typical machine includes a controlled feeder, conveyor, inspection lighting, sensors, a processing unit, air nozzles, and collection bins. The feeder spreads fragments into a thin layer. The sensors read each piece, and timed air jets push selected fragments into another stream. Small timing errors can send good glass to the reject bin.
Performance depends on more than sensor quality. Dust, wet fragments, labels, and uneven feed can affect detection, so maintenance and calibration matter. No setup catches everything. Buyers should check the machine’s performance on representative samples, including the contaminants their facility actually handles. Even a well-tuned system may need adjustments when feed composition changes.
| Machine Type | Primary Purpose | Typical Detection Method | Core Components | Typical Feed and Application | Key Consideration |
|---|---|---|---|---|---|
| Color Optical Sorter | Separates glass by visible color, such as clear, green, and amber. | RGB or other visible-light cameras capture the color of individual glass pieces; image-processing software compares readings with configured acceptance criteria. | Feed hopper, vibrating feeder, conveyor or chute, illumination system, camera, image processor, air-ejector valves, and collection bins. | Cleaned, size-graded cullet in container-glass recycling and color-specific batch preparation. | Consistent presentation and suitable particle sizing help reduce overlap and improve reliable detection. |
| Ceramic, Stone, and Porcelain (CSP) Sorter | Removes non-glass particles that can remain after crushing and screening. | Camera-based optical systems identify visible differences in color, brightness, or surface appearance. Some systems use additional sensors depending on the material and application. | Metering feeder, inspection zone, cameras and lighting, image-processing unit, air-ejection system, and separate reject and product chutes. | Processed container-glass cullet where ceramic fragments, stones, or porcelain could affect remelting and product quality. | Detection performance depends on particle size, surface condition, lighting, and how clearly contaminants differ from the glass. |
| Metal Contaminant Separator | Removes ferrous or non-ferrous metal pieces from glass streams. | Magnetic separation captures ferrous metals; eddy-current systems can separate conductive non-ferrous metals. The appropriate method depends on the metal and feed. | Magnet or magnetic drum, or an eddy-current rotor and conveyor, plus feed-control and collection equipment. | Mixed cullet and recovered glass streams that may contain wire, caps, or other metal fragments. | Magnetic and eddy-current equipment separates metals; it does not sort glass by color. |
| X-ray-Based Sorter | Separates selected contaminants or glass fractions that differ in X-ray response from the surrounding material. | X-ray transmission measurements identify differences related to material density and composition; the sorting criteria must be configured for the specific feed. | X-ray source, detector array, material-transport system, shielding, image-processing controls, and mechanical or air-ejection unit. | Specialized cullet applications where optical appearance alone does not provide adequate separation. | Performance depends on contaminant composition, particle thickness, overlap, and the sorter’s validated application settings. |
| Size-Grading Screen | Classifies glass particles into size ranges and removes undersize or oversize material. | Mechanical screening separates particles according to aperture size; it does not identify glass color or material composition. | Screen deck or vibrating sieve, mesh panels, drive unit, feed chute, and separate size-fraction outlets. | Crushed glass before or after optical sorting, where a controlled particle-size range is needed. | Screen openings, feed rate, and particle shape influence the resulting size fractions. |
| Combined Optical Sorting Line | Performs more than one separation task, such as color sorting and contaminant removal, in a coordinated process. | Uses one or more sensor types, such as visible-light cameras and application-specific additional sensors. | Feed and distribution equipment, sensor modules, control software, compressed-air supply, ejectors, conveyors, and product and reject outlets. | Recycling facilities processing cullet that requires multiple quality-control stages. | System layout should match the feed’s particle size, throughput needs, contaminant profile, and required product quality. |
