
10 Best CNC Panel Bender Manufacturers for Global Buyers
Choosing among the 10 Best Cnc Panel Bender Manufacturers for Global Buyers takes more than comparing advertised speed. A Cnc Panel Bender can form return flanges, short hems, and complex profiles with minimal manual handling. Yet results depend on part geometry, material thickness, tooling, and operator workflow. A machine that suits a high-volume appliance line may not fit a job shop’s changing orders.
The International Federation of Robotics reported 4,281,585 industrial robots operating in factories worldwide in 2023, in its World Robotics 2024 report. That figure reflects broader factory automation, not panel bender sales. Still, it shows why buyers increasingly assess machines as part of connected production. For a panel bender, check usable panel dimensions, automatic tool changes, programming support, service coverage, and integration options. Ask for a live demonstration using your own part drawings.
Quality expert W. Edwards Deming offered a useful manufacturing principle: “It is not enough to do your best; you must know what to do, and then do your best.” Applied here, that means defining the work before ranking suppliers. Published specifications can be hard to compare. Some details only become clear on the shop floor. A sharp return flange, a delicate coated surface, or a frequent changeover can expose gaps in a seemingly impressive specification. This guide compares ten manufacturers through practical buyer criteria, while recognizing that no single machine fits every factory. Review the evidence, test representative parts, and verify local support before deciding.
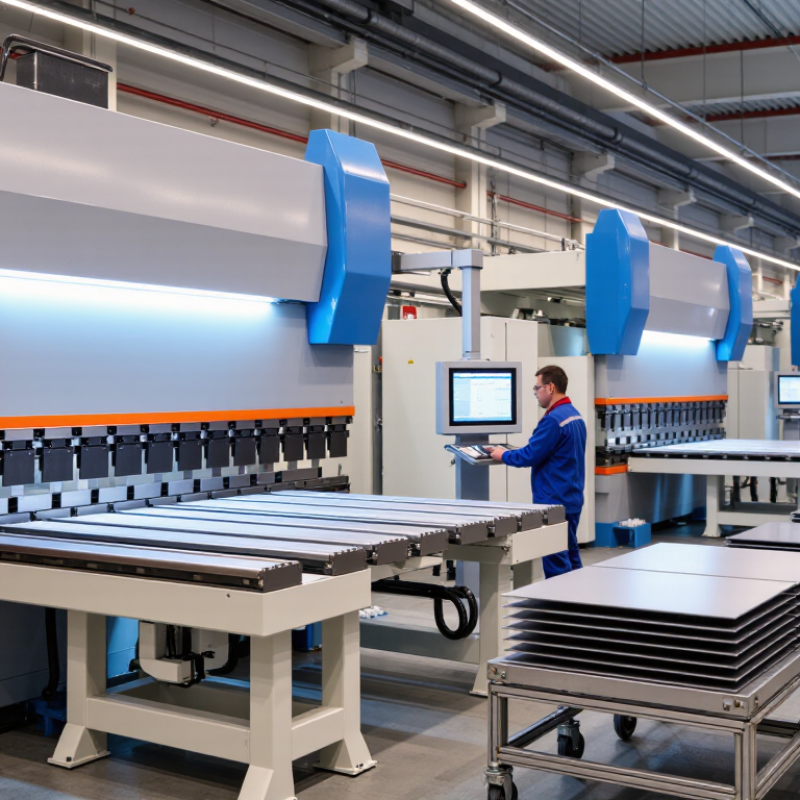
CNC Panel Benders: Operating Principles, Axes, and Sheet-Metal Applications
A CNC panel bender forms sheet metal through controlled clamping and bending. The operator loads a flat blank, and a clamp holds it against the machine table. Bending blades then move the sheet edge to the programmed angle. Depending on the machine, axes may position the back gauge, move the blades, rotate tooling, or handle the part. Their coordinated motion helps produce repeatable bends, but axis names and layouts vary by design.
Panel benders suit enclosures, cabinet doors, appliance panels, and other parts with multiple flanges. A programmed sequence can reduce manual repositioning and help maintain consistent dimensions across a batch. Still, real sheets are not perfectly uniform. Material thickness, grain direction, and springback can shift the finished angle. A careful operator checks the first piece with a measuring tool and adjusts the program when needed. Small details matter.
