What Is the Best China Stamping Press for Global Buyers?
Choosing the best China Stamping Press for global buyers requires more than comparing tonnage and price. A press may look efficient in a catalog, yet perform differently on a real production floor. Buyers should examine the target material, thickness, part size, stroke length, working speed, and required accuracy. These details influence whether the machine can produce stable parts or create costly waste.
A reliable China Stamping Press supplier should provide clear technical drawings, load calculations, inspection records, and practical test results. Ask to see sample parts made from similar steel or aluminum. Watch the feeding system, observe the noise level, and check how quickly operators can adjust the tooling. Safety guards, emergency stops, electrical protection, and documented quality controls also deserve close attention. Certifications can support trust, but they should not replace independent verification.
Long-term value depends on more than machine performance. Spare-part availability, remote troubleshooting, installation support, and operator training can strongly affect production continuity. A supplier with export experience may understand packaging, shipping procedures, and regional service expectations. Still, no supplier is perfect. Some buyers focus too heavily on the purchase price and underestimate tooling, maintenance, energy use, or commissioning costs. That mistake is easy to make.
Real experience matters.
This guide compares key machine types, supplier capabilities, technical specifications, and ownership costs. It also highlights questions global buyers should ask before signing an order. The best choice is not always the fastest press or the cheapest offer. It is the machine that fits the application, meets verified quality expectations, and remains supportable throughout its working life.
What Is a China Stamping Press and How Does It Work?
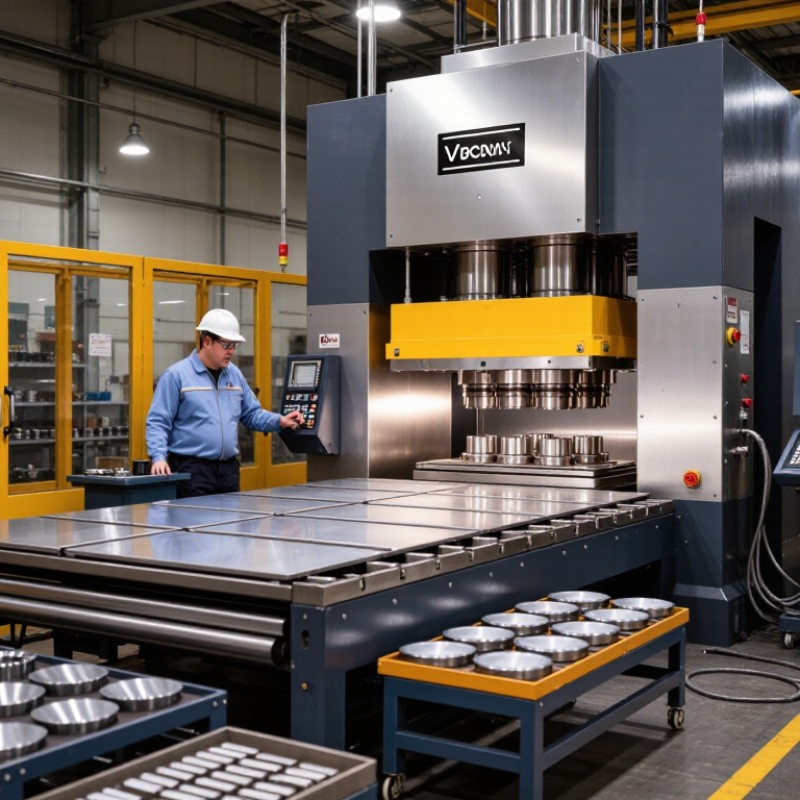
A China stamping press is industrial equipment that shapes metal sheet through controlled pressure. It uses a die, punch, frame, drive system, and control panel. The die defines the final shape, while the punch forces the sheet into or through that form.
The working cycle is straightforward but highly precise. A feeder places the metal strip beneath the punch. The press then moves downward and applies measured force. In a mechanical press, a motor stores energy in a flywheel before transferring it through a crankshaft. A hydraulic press uses fluid pressure for smoother force control. Servo systems can adjust motion more flexibly, which helps with complicated forming work.
It is not magic. Material thickness, tensile strength, die clearance, and press capacity must match. A poor match can create cracks, wrinkles, or uneven edges. In practical factory evaluations, buyers should inspect guarding, emergency stops, overload protection, and maintenance access. Ask for force charts, cycle-speed data, electrical diagrams, and operating instructions in clear English. Run sample parts before placing a large order. Watch the noise, vibration, and repeatability during continuous operation. These details often reveal more than polished photographs.
Some specifications are easy to misunderstand. “Maximum tonnage” does not always mean suitable working capacity. The useful force may depend on stroke position and speed. A reliable supplier should explain these limits honestly and provide test records. The buyer should still verify them independently, because assumptions can become expensive mistakes.
What Is the Best China Stamping Press for Global Buyers? - What Is a China Stamping Press and How Does It Work?
| Press Type | How It Works | Typical Capacity | Typical Stroke Rate | Best Applications | Main Advantages | Important Limitations | Global Buyer Checks |
|---|---|---|---|---|---|---|---|
| Mechanical Stamping Press | An electric motor rotates a flywheel. A clutch, crankshaft, and connecting rod convert rotary motion into the reciprocating motion of the slide. | Approximately 25–1,000 metric tons | Approximately 30–300 strokes per minute, depending on capacity and stroke length | Blanking, punching, bending, embossing, and high-volume progressive-die production | High production speed, repeatable motion, and relatively low operating cost per part | Force and energy are concentrated near the bottom of the stroke; less flexible for deep drawing and variable motion profiles | Verify rated tonnage at the required shut height, flywheel energy, clutch type, die space, and overload protection |
| Hydraulic Stamping Press | Hydraulic cylinders apply force through pressurized fluid. Pressure, slide position, dwell time, and speed can be controlled throughout the stroke. | Approximately 50–2,000 metric tons or more | Approximately 5–50 strokes per minute for many forming operations | Deep drawing, forming thick sheet, low-volume production, and large or complex parts | Full force is available throughout the stroke; flexible pressure and speed control; suitable for deep forming | Generally slower than mechanical presses and may require more maintenance for hydraulic systems | Check pump flow, maximum pressure, cylinder sealing, oil filtration, cooling, and emergency-stop functions |
| Servo Mechanical Press | Servo motors drive the slide directly or through a mechanical transmission, allowing programmable speed, position, acceleration, and dwell profiles. | Approximately 50–1,000 metric tons | Approximately 20–150 strokes per minute, depending on the programmed motion | Complex forming, automotive-style panels, precision parts, and processes requiring reduced noise or optimized energy use | Flexible motion control, improved forming quality, lower idle energy consumption, and reduced mechanical shock | Higher purchase cost and greater dependence on drive electronics, software, and technical support | Confirm servo motor rating, controller language, spare-parts availability, software access, and remote service capability |
| Pneumatic Auxiliary System | Compressed air operates feeding equipment, die cushions, ejectors, safety devices, or small auxiliary actuators; it is not normally the primary source of high stamping force. | Usually used for auxiliary functions rather than main press tonnage | Depends on the connected equipment and air system | Material feeding, part ejection, die cushioning, clamping, and automation | Fast response, simple control, and convenient integration with automated production lines | Compressed-air consumption, noise, and limited force compared with hydraulic or mechanical main drives | Check air pressure, flow rate, filtration, moisture control, noise level, and compatibility with the factory air supply |
| Standard Stamping Cycle: coil or blank loading → material positioning → die closing → forming, blanking, or piercing → die opening → part ejection → inspection and repeat | |||||||
| Key Sizing Data | Select capacity using material strength, thickness, part perimeter, forming depth, die design, and a safety margin. Also verify maximum stroke, shut height, slide dimensions, bolster dimensions, throat depth, and allowable die weight. | ||||||
| Safety and Compliance | Request documented risk assessment, guards, two-hand controls or light curtains where applicable, emergency stops, overload protection, electrical schematics, operating instructions, and conformity documentation suitable for the destination market. | ||||||
| Best Choice for Global Buyers | A mechanical press is generally suitable for fast, repetitive blanking and punching; a hydraulic press is generally better for deep drawing and high flexibility; a servo press is preferable when programmable motion, forming quality, and energy optimization justify the higher investment. | ||||||
